Grain moisture reconditioning can sound like a simple way to recover value from grain that dried below its preferred sale moisture. But adding or redistributing moisture is not automatically profitable, and it is not the same as running an aeration fan. The right decision depends on the grain’s condition, buyer specifications, safe handling options, and the full cost of the change. Before estimating a possible return, separate moisture equalization from intentional rewetting and account for quality and storage risk.
Contact us to discuss your grain handling setup
What does grain moisture reconditioning mean?
The phrase can describe more than one process. Grain may be called “reconditioned” when moisture within a lot redistributes and readings become more uniform after drying or handling. In other situations, a farmer may mean intentionally raising the moisture content of grain that has become too dry for a preferred market or use. Those are different jobs with different risks.
Moisture equalization does not add water to the grain lot. It gives moisture already present more time to move between kernels and parts of the grain mass. A sample taken soon after drying may not represent the whole lot evenly, so a later sample can read differently. The actual result depends on the grain, drying and handling history, temperature, and how and where the sample is taken.
Intentional rewetting is different: water is added, or wetter grain is blended with drier grain, to reach a higher average moisture content. This changes the amount of water in the lot and requires careful mixing, measurement, and management. It may be restricted by a buyer’s contract or facility rules, and uneven moisture can create quality and storage problems.
Before acting, be specific about the goal. Are you waiting for a more representative moisture reading? Trying to reduce overdrying? Looking to meet a buyer’s moisture specification? Or trying to restore moisture after grain dried too far? The answer changes which options make sense.
How can grain moisture reconditioning affect stored grain value?
Moisture can affect both the amount of grain sold and its condition. Drying removes water, so overdrying can mean selling less weight than would have been present at a higher moisture level. Depending on the buyer and contract, moisture outside the accepted range may also lead to a price adjustment, rejection, or extra handling. On the other side, grain that is too wet for its intended storage or sale plan may need more drying and may be at greater risk if managed poorly.
That is why a moisture target should not be selected from a generic rule of thumb alone. Check the specific contract, elevator or processor requirements, intended storage period, and the condition of the grain. Commodity, grade, temperature, damage, foreign material, and the buyer’s measurement method can all matter. Confirm current requirements with the buyer before spending money or changing the lot.
It is also important to distinguish a moisture reading from a quality assessment. A meter reading is one input. It does not tell you by itself whether the entire bin is uniform, whether kernels are damaged, or whether the grain can safely be held under the conditions in that bin. A useful starting point is representative sampling and a repeatable measurement routine. This guide to choosing a grain moisture meter for harvest decisions can help frame the equipment question, but the instrument must be suitable for the grain and used according to its instructions.
When might reconditioning be worth evaluating?
It may be worth evaluating when measured moisture is below a buyer’s accepted target, the expected price or weight difference is meaningful, and you have a controlled way to achieve a uniform result without compromising quality or safe storage. It can also make sense to investigate whether a reading taken soon after drying is representative before deciding that moisture must be added.
Start by comparing realistic alternatives. Those may include selling the grain as-is, waiting for moisture to equalize and sampling again, blending lots if the buyer allows it, or using a controlled reconditioning method that is appropriate for the grain and facility. In some cases the simplest answer is to accept the current condition rather than add complexity and risk.
Do not assume that a higher moisture reading automatically means a higher return. Added water increases gross weight, but the buyer may calculate settlement differently, charge for handling or drying, apply quality discounts, or reject grain that does not meet contract requirements. A potential gain on paper can disappear once those costs and conditions are included.
How do you estimate the value before changing moisture?
Use a farm-specific calculation with actual lot size, measured moisture, buyer terms, and the costs of the method under consideration. The following steps make the estimate easier to check:
- Confirm the baseline. Record the grain type, lot size, current moisture, temperature, grade or quality concerns, and sampling method. Take representative samples from appropriate locations rather than relying on a single convenient spot.
- Get the target in writing. Ask the buyer or end user for the accepted moisture range, how moisture is measured, and how settlement changes outside that range. Confirm whether blending or reconditioning is permitted.
- Estimate the physical change. Determine how much water or wetter grain would be needed using a method appropriate to the lot. Treat any calculation as an estimate, not a substitute for a validated process and repeated testing.
- Calculate gross value, then subtract costs. Compare expected settlement at the current condition with the settlement that might apply after the change. Include water, labor, energy, equipment, handling, testing, drying, and any storage or quality risk.
- Stress-test the result. Recalculate with less favorable assumptions: a smaller price difference, additional handling, a less uniform result, or a delay in sale. If a small change makes the plan unprofitable, the expected return is fragile.
A basic mass-balance calculation can help illustrate why water addition changes weight. For an idealized lot where dry matter stays constant, the estimated final grain weight is the initial dry matter divided by one minus the target moisture fraction. The example below assumes moisture percentages are on a wet basis. For example, a 10,000-pound lot at 13% moisture contains about 8,700 pounds of dry matter. At a theoretical 15% target, the final weight would be about 10,235 pounds, or roughly 235 pounds more than the starting weight.
This example is only arithmetic, not an operating recommendation. It assumes accurate initial measurements, even distribution, no grain loss, and a valid target. It does not account for settlement rules, drying charges, quality changes, or whether the process is suitable for the bin and grain. Do not use the calculation by itself to decide how to add water or how long to store treated grain.
| Option | What it can do | Costs and risks to check | Useful first question |
|---|---|---|---|
| Sell as-is | Moves the lot without further moisture handling. | Possible moisture adjustment, discount, or lost opportunity under the buyer’s terms. | What is the actual settlement at today’s measured condition? |
| Wait and sample again | May clarify whether readings have equalized after drying or handling. | Time, continued storage exposure, and the possibility that the result does not change enough. | Was the sample taken at a representative time and location? |
| Blend lots | May produce a different average moisture if blending is allowed and properly managed. | Buyer restrictions, mixing equipment and labor, unevenness, and impact on grade or quality. | Does the buyer permit this, and how will the combined lot be measured? |
| Controlled moisture reconditioning | Can raise moisture toward a chosen target when an appropriate process is available. | Equipment, water, labor, energy, uniformity, quality, storage, and compliance with buyer terms. | What validated method will achieve a uniform, measurable result? |
What should you check before adding moisture?
First, confirm that the grain is a suitable candidate and that the planned process is appropriate for its intended use. The condition of the lot matters as much as the average moisture. Existing hot spots, damaged grain, fines, insects, or signs of deterioration can change the risk. If there are concerns about grain condition, get qualified local or technical advice before attempting to raise moisture.
Second, plan for uniformity. A single average reading can hide wetter and drier zones. Uneven application or blending can leave parts of a lot at different moisture levels, making storage management and sale decisions harder. Decide how the grain will be mixed, how representative samples will be taken afterward, and what readings would prompt you to pause or change the plan.
Third, consider the storage window. Raising moisture is not just a value decision at the scale; it changes the conditions you must manage while the grain is held. Storage duration, temperature, airflow, grain condition, and the ability to monitor the lot all affect the plan. A reconditioning step should not be treated as a reason to ignore routine inspection or monitoring. For university-based agricultural guidance alongside buyer and facility requirements, consult North Dakota State University. Farm Shop MFG’s guide on keeping grain from spoiling in on-farm storage offers related storage considerations.
Finally, document the before-and-after readings, date, sample locations, method, and any quality observations. Good records help you see whether the change produced a uniform result and make the next decision with better information. They also help explain the lot’s handling history when you discuss it with a buyer.
How should you compare the settlement at two moisture levels?
Keep the comparison on the same basis. Write down the expected net proceeds if you sell the grain in its current condition, then compare that with the estimated net proceeds after the proposed change. Use the same lot, delivery date assumption, buyer, and price basis where possible. If the buyer gives you a settlement estimate, ask which moisture reading and adjustment rules it uses. A quoted price per bushel is not enough if moisture deductions, drying fees, or other charges change between scenarios.
Separate weight from price. An increase in gross weight from added water does not necessarily translate one-for-one into saleable bushels or dollars. Buyers may apply standard moisture adjustments or other contract terms. Ask how the delivered quantity is calculated and what deductions could apply. If a buyer cannot estimate the result before you change the lot, treat the expected revenue as uncertain rather than filling in a favorable number.
Include any cost that would occur only because you chose to recondition. That could mean extra loading, mixing, testing, or a second trip to a delivery point. Then compare the net difference, not just the theoretical gross value. For example, if the expected settlement improves by a modest amount but added handling and drying consume most of it, the remaining return may not justify the time or risk.
It can help to make three scenarios: a conservative case, a likely case, and an optimistic case. Use the conservative case to decide whether the project is worth pursuing. If the optimistic case is the only one that works, confirm every assumption with the buyer and the person responsible for the handling process before proceeding. Do not treat the mass-balance example above as a price forecast; it estimates physical weight only, not the amount a buyer will pay.
Which costs belong in the reconditioning estimate?
Separate one-time costs from costs that change with the amount of grain. Equipment rental or purchase, setup, and any modifications may be fixed costs for the job. Labor, water, energy, mixing, sampling, additional drying, and handling may rise with the lot size or number of passes. Include the cost of moving grain to another location if that is part of the plan. A method that looks economical for a large uniform lot may not pay for a small lot that requires the same setup.
Consider timing, too. Reconditioning may add days to the handling schedule or delay delivery. If the price window changes, the buyer’s receiving schedule fills, or the grain needs to be moved again, the expected gain may shrink. A fair comparison looks at the net sale proceeds on the same timeline, not a theoretical higher price with no allowance for the time and work needed to reach it.
Risk deserves a line in the estimate even when it is difficult to assign a precise dollar amount. Ask what happens if moisture is not uniform, if a portion fails to meet the target, or if extra drying is needed before delivery. Consider whether you can segregate and manage the affected lot rather than putting a whole bin at risk. A conservative plan identifies a maximum spend and a condition that means stop, resample, or seek advice.
Should you recondition an entire bin or a smaller lot?
The size and uniformity of the lot can change the economics. If a bin contains grain from different fields, harvest dates, or drying runs, one average moisture number may conceal meaningful variation. Before treating the bin as one consistent lot, consider whether separate loads or zones can be sampled and identified. A smaller, well-defined lot can make a trial easier to evaluate, but it still needs a suitable process and buyer approval.
Handling a portion separately may also limit exposure if the result is uncertain. Compare the cost of segregating and testing that portion with the possible benefit and any additional equipment time. Keep records that tie each sample to the relevant load or location; otherwise, before-and-after readings may not tell you whether the process worked. Avoid mixing lots simply to reach a target average unless the buyer permits it and the resulting grain can be handled consistently.
Does aeration recondition grain moisture?
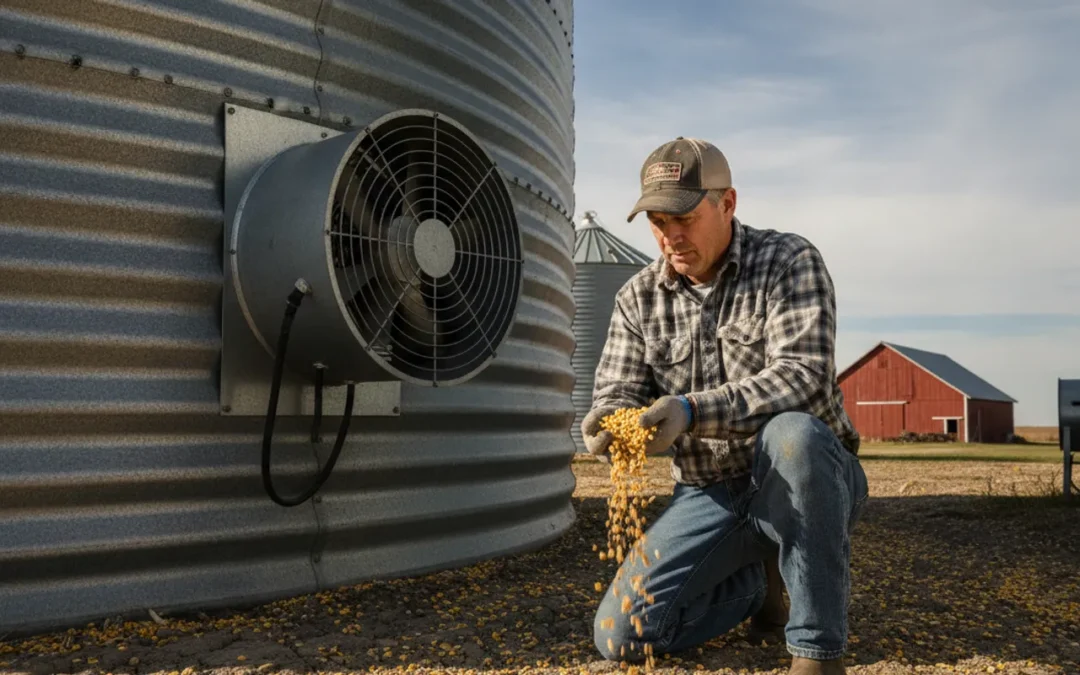
Aeration and intentional rewetting are not interchangeable. A fan moves air through grain. Depending on ambient conditions and the grain, that airflow can change grain temperature and may affect moisture distribution. It does not inject water into grain. The results depend on the air, the grain, the fan and bin setup, and the goal of the fan run.
Do not assume that running a fan will reliably raise the average moisture of an overdried lot to a specific sale target. Nor should you use a fan plan designed for one storage goal as a substitute for a controlled reconditioning method. Keep the decisions separate: determine whether the grain needs temperature management, moisture equalization, or actual moisture addition, then choose an approach designed for that job.
Automated controls can help manage fan operation based on ambient conditions, but they do not remove the need to understand the goal and check the grain. EndZone fan control is designed to automate grain bin fan control based on ambient conditions. It is a control tool, not a water-addition system. Learn how Grain Temp Guard grain bin monitoring fits into a monitoring plan as well; monitoring information supports decisions, but it does not by itself measure every moisture condition in a bin.
For farmers comparing a monitoring tool with a fan controller, match each product to the task rather than treating them as the same equipment. The Grain Temp Guard product details describe its temperature-monitoring role, while the EndZone fan-control product page covers fan automation. Neither replaces representative grain sampling or the buyer’s specifications.
How do you make a practical reconditioning decision?
Use a simple sequence before changing the lot:
- Define the objective: clarify whether you need a more representative reading, moisture equalization, or a deliberate increase in average moisture.
- Verify the lot: take representative samples, check the meter and method, and note temperature and any visible quality concerns.
- Confirm the market: get the buyer’s specification, measurement procedure, and rules on blending or reconditioning.
- Compare options: price the as-is sale, waiting and resampling, blending if permitted, and a controlled reconditioning approach.
- Plan the process: identify how moisture will be distributed, checked, and monitored. Set a clear stopping point before starting.
- Recheck and record: test representative samples after the change and keep records of the readings and handling.
This sequence helps keep the decision grounded in the specific grain lot instead of an assumed moisture target. If the projected gain depends on a best-case sale price or perfect uniformity, be cautious. A conservative estimate should still make sense after realistic handling costs and the possibility of an uneven result are included.
For storage planning beyond moisture changes, Farm Shop MFG also has a guide to grain bin sensors for soybeans. Use a sensor or fan-control system as one part of a management plan, alongside sampling, inspection, and current buyer requirements.
Contact us about grain handling equipment
Frequently asked questions
Does moisture reconditioning always increase the price of grain?
No. A higher moisture reading may increase gross weight, but buyer settlement rules, drying charges, grade, quality, and handling costs determine whether the net return improves. Confirm the terms for the specific lot before acting.
Is moisture equalization the same as adding water?
No. Equalization means moisture already in the grain redistributes and readings may become more uniform over time. Intentional rewetting adds moisture or blends in wetter grain. It requires a separate process and risk assessment.
Can a grain bin fan add moisture?
A fan moves air through the grain; it does not inject water. Airflow can affect grain temperature and moisture distribution depending on ambient conditions and the setup, but it should not be assumed to raise a lot to a chosen moisture target.
How do I know whether my grain is uniform enough?
Use representative sampling and repeatable measurements from more than one appropriate location, following equipment instructions and your facility’s procedures. A single reading may not describe the whole bin. Ask a qualified grain professional for guidance if readings vary widely or grain condition is in doubt.
What is the first step if I am considering reconditioning?
Confirm the buyer’s acceptable range and settlement rules, then verify the lot’s condition and moisture with representative samples. Only after that should you compare methods and costs.
Moisture reconditioning may protect value in the right situation, but the decision only works when the target, market terms, process, and storage plan fit the grain in front of you. Measure first, run the numbers conservatively, and use a controlled approach you can verify.